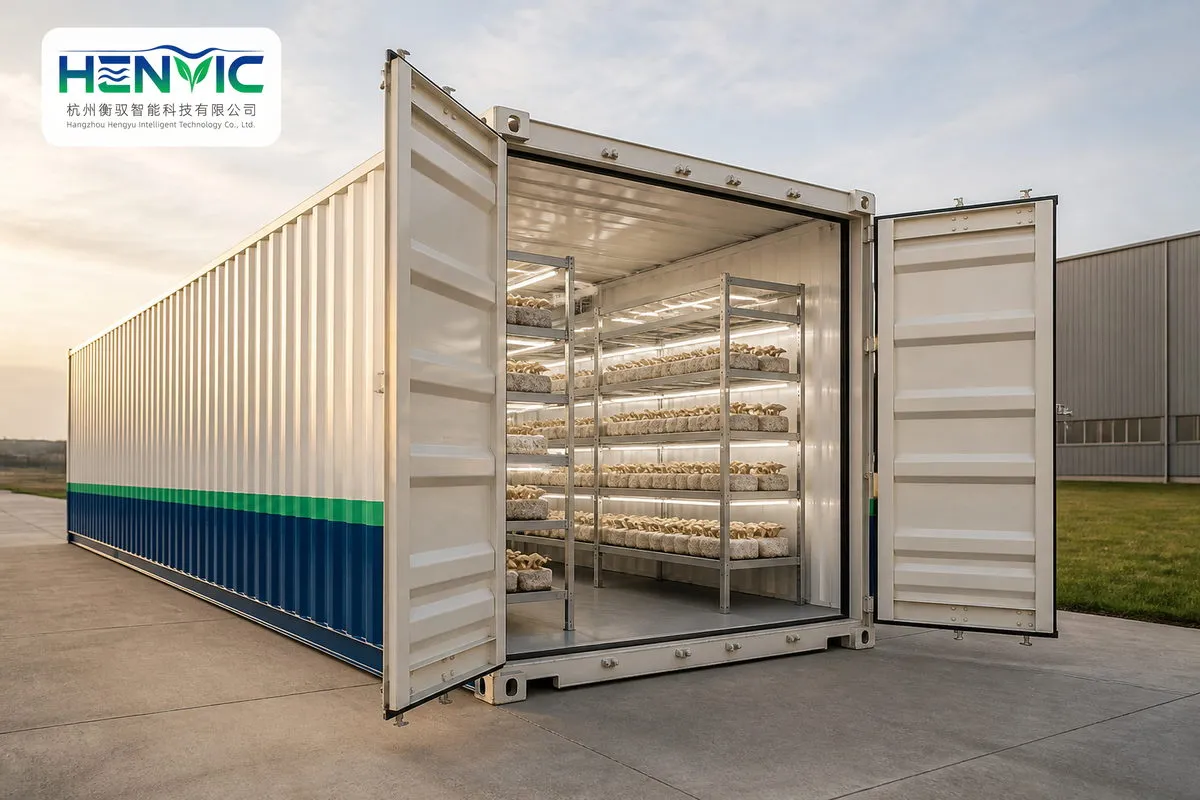
Large Mushroom Growing Chamber
The Edible Fungus Cultivation Warehouse (also known as an industrial mushroom growing warehouse or smart mushroom facility) is a fully climate-controlled, industrial-grade cultivation facility designed for medium and large edible fungus producers. Built on a standardized factory structure and equipped with an IoT cluster management system, it delivers fully automatic and precise regulation of temperature, humidity, lighting, CO₂ concentration and ventilation, supports simultaneous zoned production of multiple fungal species, and achieves an annual capacity of several hundred tonnes.
Exterior View

Modern edible fungus cultivation warehouse — a white steel-structure industrial building with a centralized rooftop ventilation system and an outdoor digital environmental display screen, surrounded by green fields and equipped with a logistics loading dock.
Interior Production Workshop

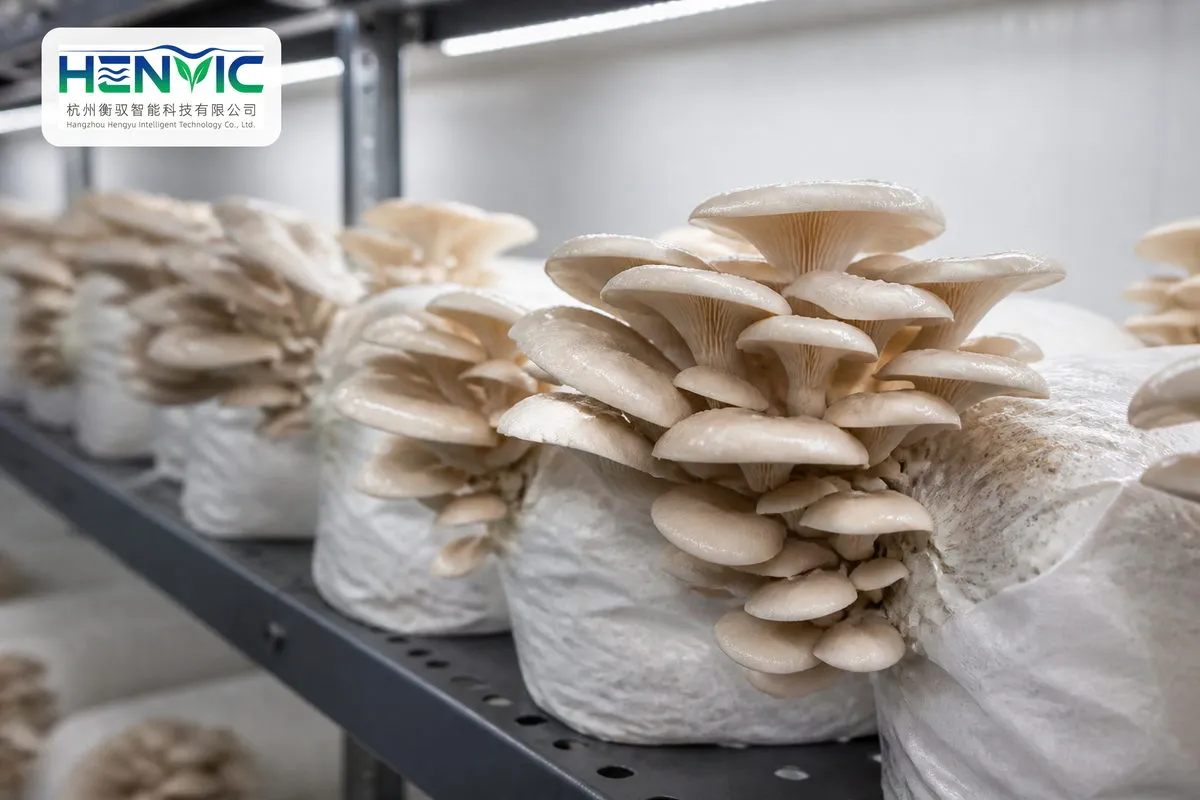
Inside the cultivation warehouse — arrays of 3 m high vertical cultivation racks densely packed with mushroom grow bags, with enoki, white beech (buna-shimeji) and oyster mushrooms cultivated simultaneously. Blue-red LED supplementary light strips provide tier-by-tier illumination, while the ultrasonic misting system sprays to maintain humidity.
Harvesting Operations

Harvesting stage — workers in clean, dust-free garments carry out manual picking. Digital sensors on the cultivation racks display real-time readings of 18.5°C temperature, 92% humidity and 850 ppm CO₂, with full environmental data records kept for every batch of mushrooms.
I. Core Parameters
| Parameter | Specification |
|---|---|
| Building type | Light steel structure / color steel panel workshop; single-bay span 8-24 m, length customizable to requirements |
| Single warehouse area | 200 m² ~ 3000 m² (customized to capacity requirements) |
| Cultivation method | Multi-tier vertical cultivation racks, 6-8 tiers, rack height 2.5-3.5 m |
| Temperature control system | Industrial chiller + heat pump, temperature range 5°C ~ 30°C, accuracy ±0.5°C |
| Humidity control | High-pressure micro-mist / ultrasonic misting humidification, range 60%-98% RH, accuracy ±3% |
| CO₂ management | Infrared CO₂ sensor + variable-frequency fresh air system, programmable threshold |
| Ventilation system | Positive-pressure supply air + return air circulation, 6-15 air changes per hour, H13 grade filtration |
| Lighting system | Full-spectrum LED grow lights, 0-100% dimmable, zoned timed control |
| Control system | Siemens/Mitsubishi PLC + industrial touch screen + IoT cloud platform |
| Remote management | Mobile app + PC web, supporting real-time monitoring, remote control and data traceability |
| Alarm system | Three-tier SMS + app + audible/visual alarms: temperature/humidity out of range, equipment fault, power failure, water supply failure |
| Data traceability | Full data storage in MySQL / cloud database, supporting multi-dimensional query and export by batch / species / date |
| Sterilization system | UV germicidal lamps + ozone generator, automatic disinfection between crop cycles |
| Annual capacity | Single warehouse (1000 m²): 150-250 tonnes of oyster mushroom per year, 100-180 tonnes of enoki mushroom per year |
| Suitable species | Oyster mushroom, shiitake, enoki mushroom, king oyster mushroom, white beech mushroom, crab-flavored mushroom, lion's mane mushroom, reishi (Ganoderma lingzhi) and others |
| Power configuration | 380V three-phase five-wire, installed capacity 80-200 kW (depending on floor area and cooling capacity) |
| Reference construction cost | ¥800-1500/m² (including civil works + equipment + installation, excluding land cost) |
II. Growth Environment Parameter Table
| Growth stage | Cycle | Temperature | Humidity | Light | CO₂ |
|---|---|---|---|---|---|
| Mycelium incubation | 20-30 days | 22-26°C | 60-70% | Darkness | <5000 ppm |
| Post-maturation | 5-10 days | 20-24°C | 65-75% | Darkness | <4000 ppm |
| Primordium induction | 3-5 days | 16-20°C | 85-95% | 500-1000 lux | <2000 ppm |
| Fruiting body development | 5-15 days | 15-22°C | 85-98% | 800-2000 lux | <1000 ppm |
| Harvest stage | 2-3 days | 14-18°C | 80-90% | 500-1000 lux | <1500 ppm |
| Between-flush period | 7-10 days | 20-24°C | 70-80% | Weak light | <3000 ppm |
Note: The figures above are general reference values. Fine adjustments are required depending on the specific variety and regional climate conditions.
III. Core Advantages
1. Round-the-Clock Intelligent Control
- Industrial PLC + IoT dual-redundant control architecture; local automatic operation continues unaffected in the event of a network outage
- Preset multi-species growth parameter templates — switch species with one touch without setting each parameter manually
- AI self-learning algorithm: automatically optimizes temperature and humidity curves based on historical yield data
2. Cleanroom-Grade Production Environment
- Fresh air system fitted with H13 high-efficiency filters, achieving class 10,000 cleanroom standards in the workshop
- Alternating UV and ozone disinfection, executed automatically between crop cycles to effectively prevent cross-infection by competing microorganisms
- Positive-pressure air supply design prevents external contaminants from entering
3. High-Density Vertical Cultivation
- 6-8 tier vertical cultivation racks delivering 5-8 times the yield per unit area of a conventional greenhouse
- Optional rail-based logistics conveyor system automates loading and unloading of grow bags, saving 60% of labor
- Modular rack design allows flexible adjustment of tier height and spacing
4. Full-Chain Digital Traceability
- Environmental parameters recorded throughout the entire process for every batch, from spawn bag inoculation to finished product dispatch
- Scan the code to trace the full growth history, meeting the quality inspection requirements of premium supermarkets and export markets
- Data dashboard supports multi-dimensional visual analysis of yield, energy consumption and equipment operating efficiency
5. Energy-Saving and Cost-Reduction Design
- Variable-frequency fans automatically adjust speed according to CO₂ concentration, saving over 30% in energy
- Waste heat recovery from the chiller unit is used for winter heating and pre-heating during grow bag sterilization
- LED supplementary lighting is controlled by zone and time period according to growth stage, reducing electricity waste
IV. Comparison with Conventional Cultivation Models
| Dimension | Smart cultivation warehouse | Conventional greenhouse | Container module |
|---|---|---|---|
| Single unit area | 200-3000 m² | 200-1000 m² | Approx. 30 m² |
| Annual production cycles | 8-12 flushes | 2-4 flushes | 8-10 flushes |
| Yield per unit area | Very high | Low | High |
| Environmental control accuracy | ±0.5°C / ±3% RH | Extensive, with large fluctuations | ±0.5°C / ±3% RH |
| Labor requirement | 2-5 people per 1,000 m² | 5-10 people per 1,000 m² | 0.5-1 person per module |
| Contamination rate | <1% | 5-15% | <2% |
| Product consistency | Very high | Low | High |
| Land use efficiency | ★★★★★ | ★★☆ | ★★★★ |
| Initial investment | ¥800,000-1,500,000 per 1,000 m² | ¥30,000-80,000 per 1,000 m² | ¥150,000-500,000 per module |
| Digitalization level | Full-chain data traceability | Largely dependent on manual work | Fully automated |
V. Return on Investment Estimate (Example: 1,000 m² Cultivation Warehouse)
| Item | Data |
|---|---|
| Construction cost | ¥800,000-1,500,000 (including civil works + climate control equipment + cultivation racks) |
| Annual capacity | Oyster mushroom 150-250 tonnes / enoki mushroom 100-180 tonnes |
| Market reference price | Oyster mushroom ¥6-10/kg, enoki mushroom ¥8-15/kg |
| Annual output value | ¥900,000 ~ ¥2,500,000 |
| Annual operating cost | ¥400,000-800,000 (electricity + grow bags + labor + packaging + logistics) |
| Annual net profit | ¥500,000 ~ ¥1,700,000 |
| Payback period | 1.5-3 years |
Note: The data above represents industry reference ranges. Actual returns are influenced by factors such as species selection, market conditions and management capability. A detailed feasibility study based on local market research is recommended.
VI. Construction Scope Checklist
| Module | Contents | Remarks |
|---|---|---|
| Civil works | Building foundations, steel structure, color steel panel envelope, epoxy resin flooring | Executed in accordance with building codes |
| Refrigeration system | Industrial chiller, cooling tower, chilled water pump, pipe insulation | Selected based on heat load calculations |
| Humidification system | High-pressure micro-mist main unit, stainless steel piping, atomizing nozzles | Independent zoning for each tier of cultivation rack |
| Ventilation system | Variable-frequency centrifugal fans, high-efficiency filters, air ducts, motorized air valves | Positive-pressure supply air + return air |
| Lighting system | Full-spectrum LED light strips, dimmable driver power supplies, time control modules | Zoned programmable control |
| Cultivation racks | Hot-dip galvanized steel frames, grow bag trays, drip irrigation piping | Height and tier count customizable |
| Control system | PLC control cabinet, touch screen, sensors, actuators | Siemens / Mitsubishi and other brands |
| Software platform | IoT cloud platform, mobile app, data dashboard | Includes first-year service fee |
| Auxiliary equipment | Sterilizer, inoculation machine, packaging machine, cold storage | Configured according to production capacity |